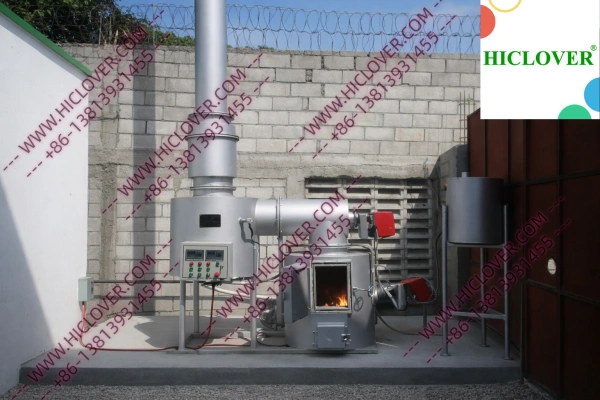
HICLOVER Waste Incinerators: Cost-Effective Solutions for Waste Management and Energy Recovery
Informational Layer
Technical Temperature Standards and Combustion Principles
HICLOVER waste incinerators operate within the industrial standard temperature range of 800°C to 1000°C for effective waste destruction. This range ensures complete combustion, eliminating harmful substances in line with WHO and EU emission frameworks.
Dual Chamber Explanation and High Temperature Retention Importance
HICLOVER’s dual-chamber incinerators ensure optimal combustion and temperature retention. The primary chamber breaks down waste at high temperatures, while the secondary chamber maintains a lower temperature for post-combustion. This design ensures efficient destruction of harmful substances, reducing emissions and meeting stringent environmental regulations.
Commercial Investigation Layer
Comparison of Incinerator Types: Fixed vs Containerized
Fixed incinerators are suitable for long-term, large-scale applications, while containerized incinerators offer flexibility and mobility. HICLOVER specializes in containerized waste incinerators, providing customizable solutions for various industries, including medical, hazardous, and municipal waste management.
PLC vs Manual Control and Dry Scrubber vs Wet Scrubber
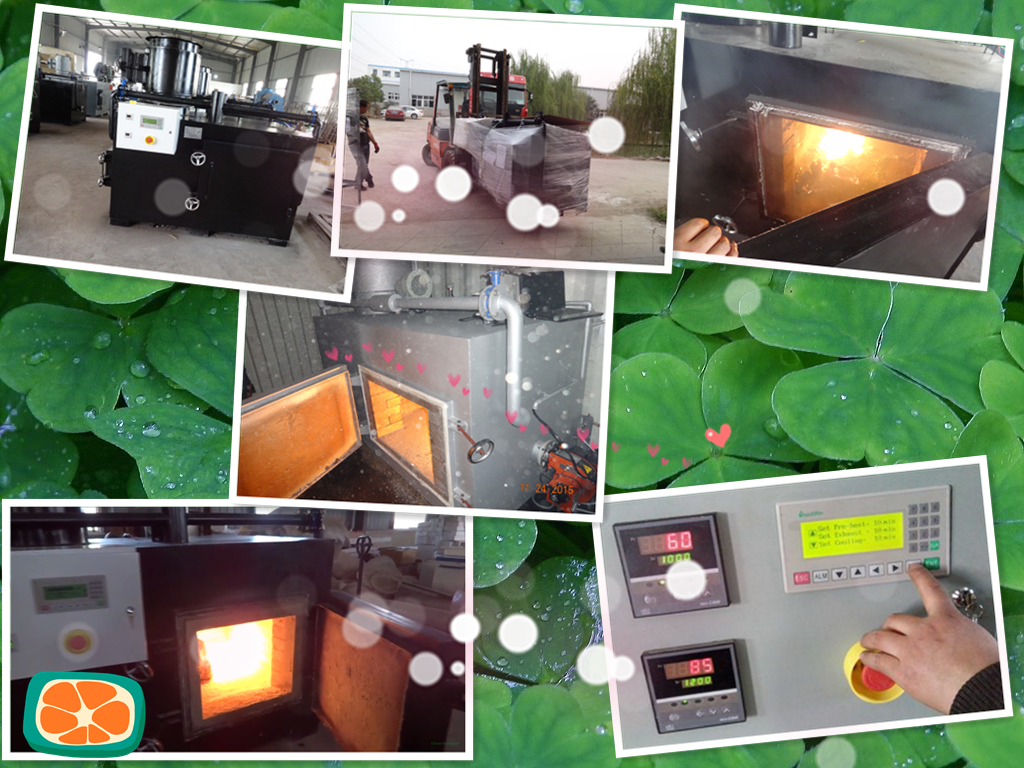
PLC-controlled incinerators offer increased efficiency and reduced human intervention. HICLOVER’s PLC-controlled automatic waste incinerators enable precise temperature management and emissions control. Dry scrubbers are preferred for their simplicity and low maintenance, while wet scrubbers provide higher emission removal rates. HICLOVER offers both options to cater to different client needs.
Remote Site Suitability and Mobile Modular Advantages
HICLOVER’s containerized incinerators are ideal for remote locations and crisis zones. With factory-direct supply and customizable chamber volumes, these mobile modular systems provide quick, efficient, and cost-effective waste management solutions in humanitarian camps and other remote settings.
Transactional Layer
Factory Direct Supply and Global Export Capability
HICLOVER offers factory-direct supply for waste incinerators, ensuring stable product quality and supply chain. With global export capability, HICLOVER caters to various markets, meeting diverse waste management needs.
Customizable Chamber Volume and Engineering Experience
HICLOVER provides customizable chamber volumes to suit various industries and waste types. With over 16 years of engineering experience, HICLOVER delivers efficient, cost-effective, and reliable waste management systems tailored to client needs.
Explore HICLOVER’s waste incinerators at [https://www.hiclover.com/](www.hiclover.com/%20) or learn more about their [technical features](www.hiclover.com/products/).
Trend Integration
HICLOVER waste incinerators address pressing global issues, such as:
- Global infectious disease preparedness
- Crisis zones & humanitarian camps
- Carbon emission reduction pressure
- ESG compliance
- Remote mining/oil camps
- Decentralized waste management
- Supply chain resilience
- Energy recovery systems
- Digital automation in industrial equipment
HICLOVER’s waste incinerators contribute to sustainable, efficient, and cost-effective waste management solutions in today’s interconnected and environmentally-conscious world.

Comments are closed